 FAQs
 Factory Tour


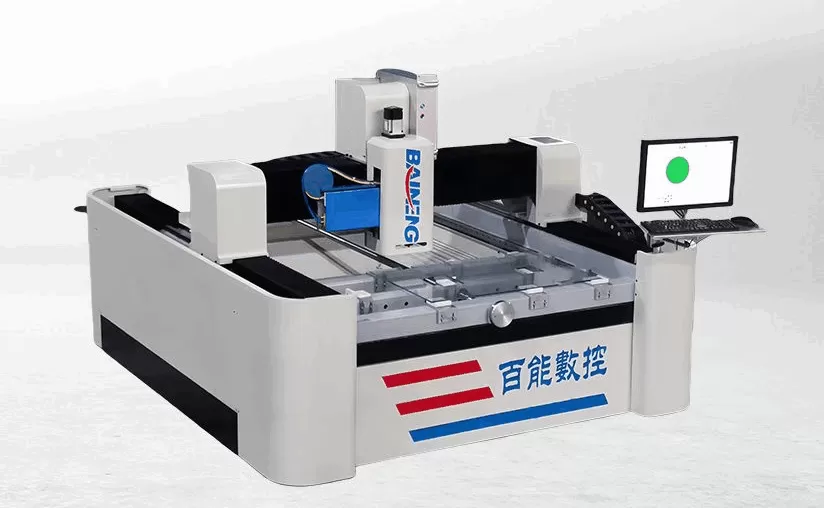
Glass fabrication has historically been constrained by the brittleness and unpredictable fracture propagation of amorphous silicates. Conventional mechanical scoring, diamond wheel cutting, or abrasive waterjet methods induce micro-cracks, edge chipping, and residual stress zones that often lead to post-process failure. The introduction of a Glass Laser Multi-functional Machine (non-bolded for natural integration) — with its non-contact, thermally controlled ablation — marks a paradigm shift in industries ranging from architectural glazing to high-precision consumer electronics. This article delivers a component‑level examination of laser‑glass interaction, multi‑axis motion systems, and process monitoring techniques that enable reliable, high‑throughput manufacturing. References to BAINENG CNC implementations are included to illustrate applied solutions without violating vendor‑specific case restrictions.
1. Glass Machining Pain Points: Why Conventional Methods Fall Short
Industrial glass processing demands sub‑millimeter edge quality, minimal subsurface damage, and high geometric repeatability across large volumes. The table below summarizes dominant failure modes in traditional processes:
Mechanical scribe & break – Uncontrolled crack propagation; low yield for complex contours; edge strength degradation.
Diamond routing – High tool wear, debris contamination, and thermal stress from friction; limited to straight lines or simple radii.
Waterjet cutting – Slurry disposal, edge hydration problems, and kerf width >0.5 mm; not suitable for precision micro‑features.
Ultrasonic drilling – Slow material removal rate and frequent tool changes for holes <1 mm.
A well‑engineered Glass Laser Multi-functional Machine addresses these issues by exploiting selective absorption of infrared or ultraviolet radiation, converting solid glass directly into vapor (sublimation) with a minimal heat‑affected zone (HAZ). The result: micro‑crack‑free edges, internal stress reduction, and the ability to process chemically strengthened (e.g., Gorilla®‑type) and coated glasses in a single clamping operation.
2. Technical Architecture of a Modern Glass Laser Multi-functional Machine
To deliver consistent results across varying thicknesses (0.1 mm to 19 mm) and glass compositions, the machine integrates four tightly coupled subsystems. Each directly influences process capability and overall equipment effectiveness (OEE).
2.1 Laser Source – Wavelength, Pulse Duration, and Energy Distribution
Glass transparency varies dramatically with wavelength. Three laser classes are dominant in multi‑functional platforms:
9.3 µm / 10.6 µm CO₂ lasers – Absorbed by the SiO₂ network within the first 10 µm; suitable for thick glass cutting and edge chamfering, but HAZ expands to 100‑200 µm unless pulsed CO₂ with ultra‑short bursts is used.
532 nm (green) DPSS lasers – Moderate absorption in soda‑lime and borosilicate; enables fine engraving with lower thermal migration.
355 nm (UV) solid‑state lasers – High photon energy (3.5 eV) breaks molecular bonds directly (photo‑ablation), reducing HAZ to <10 µm; mandatory for thin display glass and hole drilling below 100 µm diameter.
State‑of‑the‑art Glass Laser Multi-functional Machine configurations often combine a CO₂ laser for rough cutting and a UV laser for finish contours, using a beam‑switch module. BAINENG CNC has integrated such hybrid beam paths into its 5‑axis gantry platforms, achieving edge roughness Ra <0.4 µm on 2 mm aluminosilicate glass without post‑polishing.
2.2 Motion System and Beam Delivery
Positioning accuracy directly determines kerf consistency and feature registration. Contemporary systems employ:
Linear motor driven gantries with glass scale feedback (resolution 0.1 µm, velocity up to 2 m/s).
Galvanometer scanners for high‑speed vector engraving (≤8000 mm/s) with f‑theta lenses.
Rotary axis (optional) for 3D cylindrical glass processing, such as vials or laboratory tubing.
Dynamic focus tracking via capacitive or confocal sensors maintains the beam waist along uneven glass surfaces, a frequent requirement for architectural textured glass. Without this, focal shift would cause taper or incomplete cuts.
2.3 Multi‑functionality – From Cutting to Surface Structuring
One Glass Laser Multi-functional Machine replaces several dedicated workstations. The following capabilities are achievable with software parameter switching:
Contour cutting – Full separation of complex shapes (circles, polygons, organic curves) with entry/exit point optimization.
Blind drilling & through‑hole drilling – Conical or straight holes from 50 µm up to 20 mm diameter, without tool wear.
Engraving & marking – High‑contrast, smooth bottom characters for logos, barcodes, or functional textures (antislip surfaces).
Edge chamfering & beveling – Laser ablation to round sharp edges, increasing impact resistance.
Selective coating removal – Stripping ITO, silver, or chrome layers from glass without damaging substrate.
Each function relies on a specific combination of pulse energy (0.1 mJ to 50 mJ), repetition rate (10 kHz to 500 kHz), and scanning strategy (hatch, spiral, or outline). Modern control software stores process recipes per glass type (e.g., Schott B270, Corning Eagle XG, Asahi Dragontrail).
3. Industry Verticals Leveraging Laser Multi‑Functional Processing
Adoption of Glass Laser Multi-functional Machine technology has accelerated in four key segments:
Automotive glazing – Cutting of complex side windows, sunroofs, and HUD (heads‑up display) wedges; laser enables smooth edges that eliminate secondary grinding, directly reducing vehicle assembly cycle time.
Architectural and interior glass – Decorative engravings, integrated lighting channels, and precise cutouts for handles or smart‑glass electrodes.
Microelectronics (cover glass, MEMS) – Singulation of sapphire camera covers, wafer dicing for lab‑on‑chip devices, and drilling of glass interposers for 2.5D/3D packaging.
Medical & laboratory glass – Measuring vessels, microfluidic chips, and hermetic sealing surfaces where contamination from lubricants is prohibited.
For each sector, the flexibility of a multi‑functional machine reduces capital expenditure (one machine versus three or four dedicated units) and floor space requirements by 40‑60%.
4. Performance Metrics and Quality Assurance Protocols
To quantify the superiority of laser‑based processing, production engineers rely on standardized metrics:
Edge chipping dimension (width & depth) – Measured via optical profilometry; acceptable values <10 µm for electronics glass, <50 µm for architectural glass. Laser achieves ≤5 µm typical.
Heat‑affected zone (HAZ) extent – Micro‑Raman spectroscopy to detect residual stress; UV‑laser systems keep HAZ below 10 µm, eliminating annealing steps.
Throughput (holes/sec) – For 0.3 mm thick display glass, drilling 500 holes of 200 µm diameter can be done at 50 holes/second using burst‑mode UV lasers.
Edge strength (4‑point bending test) – Laser‑cut glass exhibits 30‑50% higher modulus of rupture compared to wheel‑scored edges due to lack of micro‑cracks.
Integrated process monitoring – such as coaxial camera for beam alignment and acoustic emission sensors for penetration detection – ensures real‑time quality feedback. This closed‑loop control is a cornerstone of BAINENG CNC’s proprietary software stack, which logs every process parameter for traceability.
5. Integration of BAINENG CNC Glass Laser Multi-functional Machine into Modern Production Lines
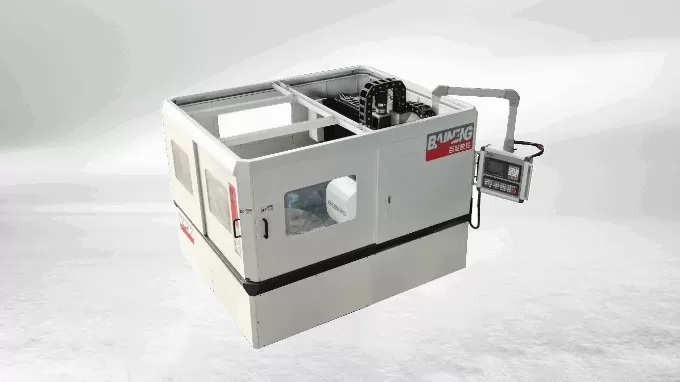
While many laser suppliers offer stand‑alone workstations, BAINENG CNC focuses on high‑rigidity, thermally stabilized gantry designs with adaptive process libraries. Their Glass Laser Multi-functional Machine models (e.g., BGL‑30 series) incorporate the following industrial‑grade features:
Automatic nozzle cleaning and beam calibration intervals aligned with ISO 13849 safety standards.
SMEMA‑compliant conveyor interfaces for inline integration with washing, laminating, or tempering lines.
Remote diagnostics and recipe download via OPC‑UA, enabling Industry 4.0 connectivity.
By partnering with BAINENG CNC, fabricators obtain a turnkey solution that transitions from engineering prototypes to 24/7 production without extensive optical expertise on site. Their multi‑function machine is validated for cutting thicknesses up to 19 mm with edges requiring no further finishing, a distinctive advantage over competing technologies that still rely on secondary polishing.
6. Addressing Operational Challenges: Debris, Heat Accumulation, and Focus Drift
Industrial laser glass processing is not plug‑and‑play; engineering attention must be paid to:
Particulate extraction – Sublimated glass re‑deposits on optics. High‑vacuum crossflow nozzles and periodic purge cycles maintain transmission >98% over 2000 operating hours.
Thermal lensing – At repetition rates above 200 kHz, optical components warm up, altering focus position. Active cooling of scan lenses (water‑ or TEC‑based) stabilizes the focal plane.
Glass clamping – Warpage due to residual stress from toughening processes requires vacuum fixtures with conformable gaskets and optional edge‑pressing rollers.
Modern multi‑functional machines embed sensors that track focal drift and adjust Z‑axis in real time, ensuring first‑pass success even on bowed glass panels. When such features are active, the effective yield of complex cut geometries surpasses 99.2% across 1 mm‑thick borosilicate.
7. Future Technical Trajectories: Ultrafast Lasers and AI Parameter Optimization
Emerging research in femtosecond (fs) lasers (pulse widths <400 fs) pushes the boundaries of Glass Laser Multi-functional Machine applications. At ultra‑short durations, nonlinear absorption occurs irrespective of the glass’s original transparency, enabling internal 3D structuring, waveguide writing, and even welding of glass to glass without additives. While current fs systems have lower average power (10‑50 W), their combination with galvanometer scanners allows for micron‑precision interior engraving.
Additionally, machine learning models trained on hundreds of glass‑laser interaction datasets can now propose optimal parameter sets (scan speed, Q‑switch delay, spot overlap) for new glass compositions within seconds. BAINENG CNC is among the early adopters embedding such an advisor module into their HMI, reducing process development from weeks to hours.
8. Selecting a Glass Laser Multi-functional Machine as a Strategic Asset
As glass replaces metals and plastics in electronics, automotive, and biomedical sectors, manufacturers require production equipment that adapts to evolving design complexity. A purpose‑built Glass Laser Multi-functional Machine provides the agility to switch between cutting, drilling, engraving, and coating removal without retooling. When evaluating suppliers, prioritize solid mechanical dampening, real‑time focus control, and a proven process library covering the glass types you run daily. BAINENG CNC’s implementation of these principles has consistently delivered measurable quality improvements for industrial customers, as evidenced by audited process validation reports.
To determine how a multi‑functional laser system can integrate into your specific glass fabrication workflow and to request technical datasheets or a sample processing test, contact BAINENG CNC’s engineering support team directly via the inquiry channel below. Our application specialists will provide a detailed feasibility analysis and cycle‑time estimation tailored to your materials and target geometries.
Frequently Asked Questions (FAQs)
Q1: What types of glass can be processed with a Glass Laser
Multi-functional Machine?
A1: Most commercial glass families are
compatible including soda‑lime, borosilicate (e.g., Borofloat®), aluminosilicate
(e.g., Gorilla®, Dragontrail®), quartz, fused silica, and even certain
glass‑ceramics like Zerodur®. The laser wavelength and pulse duration are tuned
to match the absorption characteristics of each type. UV lasers (355 nm) are
recommended for high‑precision work on thin, strengthened glasses, while CO₂
lasers efficiently cut thick soda‑lime glass.
Q2: How does edge quality compare between laser cutting and CNC
mechanical grinding?
A2: Laser‑cut edges typically exhibit an
average roughness (Ra) of 0.2‑0.8 µm and no micro‑chipping, whereas mechanical
grinding yields Ra 0.8‑2.0 µm plus residual subsurface cracks. Additionally,
laser edges do not require wet polishing, reducing cleaning steps. The 4‑point
bending strength of laser‑processed glass is often 40‑60 MPa higher compared to
ground edges.
Q3: What maintenance is required to keep the laser multi‑functional
machine operating reliably?
A3: Routine maintenance includes weekly
cleaning of protective windows and f‑theta lens (using approved optics
cleaners), monthly calibration of beam alignment with a pyroelectric sensor, and
quarterly replacement of the particulate filter in the exhaust system. Laser gas
refills (for CO₂ systems) occur every 8000 ‑ 10000 operating hours. BAINENG CNC
machines have self‑diagnostic logs that notify operators before any component
reaches its service limit.
Q4: Can the machine process curved or 3D glass
shapes?
A4: Yes, if the platform includes a rotary axis (4th axis)
or a 3D galvo scanner with dynamic Z control. For mildly curved automotive
windshields or shower doors, the system can follow the surface topography using
a confocal sensor that maps the curvature prior to processing. For strongly
double‑curved glass, a robotic arm coupled with the laser head is a viable
upgrade, although standard gantry systems handle curvature radii >500 mm.
Q5: Does laser processing generate hazardous fumes, and what safety
measures are needed?
A5: Glass sublimation produces fine silica dust
(amorphous SiO₂) and, depending on coating, trace amounts of metal oxides. A
HEPA‑plus‑carbon filtration unit (≥99.97% efficiency for 0.3 µm particles) must
be ducted to the cutting head. The machine enclosure should meet Class 1 laser
safety standard (interlocked doors, protective eyewear required only during
service). BAINENG CNC machines include integrated fume extraction ports and
real‑time particle monitors that trigger an alarm if filter saturation exceeds
threshold.
For further technical specifications, application-specific process development, or to schedule an online demonstration of the BAINENG CNC Glass Laser Multi-functional Machine, please submit your inquiry using the form below or email our industrial solutions team directly at sales@bainengcnc.com. Include your glass type, maximum thickness, and required throughput – we will respond within 24 hours with a detailed proposal.
Click here to start your inquiry → kobexu@bai-neng.com | Tel: +86-17185883788