
 FAQs
 Factory Tour


High-volume glass processing leaves no margin for unstable equipment. Production directors often install a machine marketed with high precision specs, only to watch scrap rates climb and profit margins shrink within six months.
Surface micro-fractures, beam drift during three-shift operations, and constant manual alignment quickly destroy operating budgets. In 2026, factory profitability depends on overall unit throughput rather than standalone bench speeds.
Selecting the best glass engraver for your facility requires looking beyond maximum wattage. You need a system that minimizes thermal stress, integrates directly with factory automation lines, and drives down cost per piece.
Whether you process cosmetic flacons, architectural panels, or technical borosilicate substrates, BAINENG CNC engineers commercial glass processing solutions built to hit strict cycle time targets without compromising yield. If you need to audit your current line efficiency, submit your part drawings for an engineering review and cycle time calculation.
.webp?t=1789986038943 "best glass engraver")
The Hidden Cost Trap: What Defines Commercial Success?
A low purchase price often hides severe operational expenses. When sourcing commercial glass etching equipment, procurement teams frequently focus on capital expenditure (CAPEX) while overlooking operational expenditure (OPEX).
Glass behaves differently from metals and plastics. It is brittle, possesses low thermal conductivity, and builds internal tension when heated unevenly. A system that creates rapid micro-cracking ruins downstream tempering and coating stages.
To identify the best glass engraver for continuous industrial output, calculate the following cost drivers:
Scrap Rates: Discarding 8% to 12% of finished glass due to chipping or heat shock destroys annual profits.
Secondary Finishing: If an operator must clean, deburr, or fire-polish an engraved edge, your labor cost per piece doubles.
Consumables and Masking: Traditional sandblasting demands constant abrasive replacement and film plotting, introducing recurring waste streams.
Thermal Downtime: Laser tubes with poor chiller integration suffer beam divergence after two hours of continuous firing, shifting focal points and causing production halts.
Industrial glass production requires machines that guarantee repeatable, non-contact surface alteration across thousands of cycles per shift.
Laser Physics: UV Cold Processing vs. CO2 and Sandblasting
Choosing the correct beam wavelength determines whether your factory maintains a 99% yield rate or struggles with micro-cracks. The long-standing debate of UV laser vs CO2 for glass processing centers on photothermal versus photochemical ablation.
CO2 Lasers (10.6 µm): High Speed with Thermal Strain
CO2 laser sources interact strongly with silicate glass through photothermal absorption. The beam rapidly heats the glass above its melting temperature, creating localized micro-fractures that produce a visible, frosted mark.
For thick sheet glass, industrial drinkware, and deep reliefs, CO2 systems deliver impressive linear processing speeds. However, the Heat-Affected Zone (HAZ) remains large. If you engrave thin-walled perfume containers or tempered panels, the thermal shock induced by a CO2 system can trigger spontaneous catastrophic breakage during subsequent packaging or filling.
UV Lasers (355 nm): The Cold Processing Benchmark
UV lasers utilize a short wavelength that delivers high-energy photons directly into the molecular bonds of the glass. Instead of melting the material, the 355 nm light breaks chemical bonds through cold photochemical ablation.
Because thermal transfer into surrounding areas remains negligible, the UV method eliminates micro-cracks, surface chipping, and internal tension. It produces crisp, high-contrast, smooth marks on crystal, soda-lime, borosilicate, and quartz glass.
For high-value consumer goods, medical vials, and premium optics, UV cold marking is widely considered the best glass engraver technology because it requires zero downstream cleaning and produces clean, tactile finishes.
Why Modern Plants Are Replacing Abrasive Sandblasting
Automated sandblasting historically handled deep frosting and relief art on architectural sheets. Yet industrial facilities are phasing this equipment out due to strict environmental, health, and safety (EHS) regulations.
Sandblasting creates airborne silica dust, demands continuous replacement of aluminum oxide or silicon carbide grit, and requires adhesive vinyl masks. Moving to an industrial glass laser engraving machine removes physical consumables, cuts labor, and keeps the production floor clean.
Matching Machine Configurations to Production Workflows
Different factory floors require completely different machine architectures. Choosing the best glass engraver depends entirely on your line speed, material format, and automation readiness.
Scenario A: High-Speed Beverage, Spirits, and Cosmetic Lines
High-volume packaging lines cannot afford indexing delays. Stopping a conveyor to clamp a bottle introduces structural bottlenecks.
Recommended Configuration: Marking-on-the-Fly (MOTF) UV laser systems equipped with digital high-speed galvanometer scanners.
Critical Metric: Line tracking synchronization up to 120 meters per minute with optical rotary encoders.
Key Advantage: Direct serialization, traceability QR codes, and branding applied directly to glass packaging while items move continuously on the line.
Scenario B: Large-Format Architectural and Transport Glass
Processing shower panels, structural facades, partitions, or bus side windows requires rigid frames that maintain microscopic focal depths across multiple square meters.
Recommended Configuration: Gantry-style flatbed processing centers with integrated vacuum beds and synchronized dual-drive servo systems.
Critical Metric: Positional accuracy within ±0.03 mm over a 3000 mm x 2000 mm working field.
Key Advantage: Manufacturers such as BAINENG CNC build heavy-duty mechanical gantry bases that eliminate vibration, ensuring crisp geometric lines across massive lites without optical stitching errors.
Scenario C: Technical, Semiconductor, and Laboratory Glass
Display panels, microfluidic channels, and optical glass disks demand microscopic precision without microscopic debris.
Recommended Configuration: Picosecond or femtosecond ultrafast industrial glass laser engraving machines.
Critical Metric: Pulse durations under 15 picoseconds to completely bypass thermal dissipation.
Key Advantage: Clean subsurface engraving and precise channel cutting without micro-fracturing adjacent walls.
Calculating Glass Processing ROI: The Commercial Equation
Before issuing a purchase order, your finance and production teams must validate machine payback periods. Use this standard formula to project your capital equipment return:
ROI = [(Annual Labor Savings + Consumable Reduction + Scrap Value Savings) - (Depreciation + Energy Costs)] / Total CAPEX x 100%
Consider the production data from an actual commercial retrofit below.
Case Study: Tableware Producer Modernization
A commercial stemware factory was running three shifts utilizing legacy CO2 machines alongside mechanical screen printers. The plant faced high reject rates and heavy labor costs tied to manual masking and cleaning.
Previous Equipment: 4x standalone CO2 plotters with manual hand-loading jigs.
New Solution: 2x automated UV laser workcells with integrated rotary indexing.
Scrap Rate: Fell from 11.4% to 0.4% within the first 30 days.
Labor Allocation: Reduced from 6 dedicated machine operators to 2 supervisory operators per shift.
Cycle Time: Decreased from 38 seconds to 11 seconds per glass item.
Payback Period: 5.8 months based on glass material salvage and labor redeployment alone.
When you invest in the best glass engraver for your business model, lower operational waste recovers your initial machine investment well before your first fiscal year concludes.
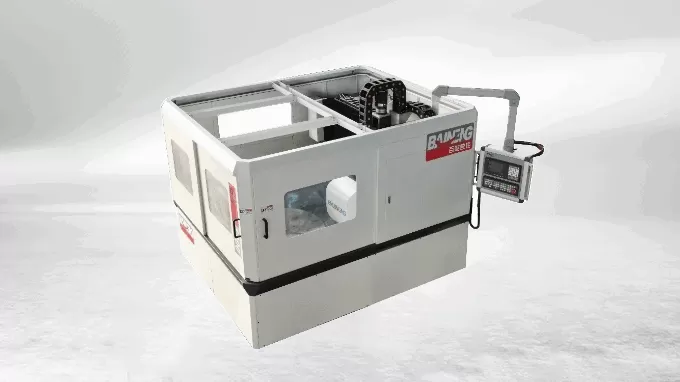
Industrial Automation: AI Vision and Robotic Material Handling
Stand-alone machines are obsolete in modern industrial architectures. Real gains come from linking factory automation glass engraving cells into your broader smart manufacturing setup.
AI Vision Positioning: Ending Physical Jigging
Glass components slide, rotate, and settle inconsistently on belts. Traditional production lines rely on machined steel jigs to lock every bottle or pane into a fixed position. These mechanical fixtures wear down, scratch polished glass, and require downtime during product switchovers.
Modern commercial glass etching equipment incorporates high-speed coaxial or look-down machine vision cameras. The software captures the product profile within milliseconds, detects rotational offsets, and recalculates the laser firing path in real time. Products can sit randomly on an open conveyor, and the machine will locate the target zone and engrave it without operator assistance.
Robotic Loading and Lights-Out Production
Integrating 6-axis articulated robots or Cartesian pick-and-place units creates a fully automated cell. Vacuum suction arrays lift delicate raw glass directly from transport pallets, seat it inside the laser enclosure, and stack finished goods straight into annealing or packaging stations.
This automated flow eliminates fingerprints, oil contamination, and operator-induced drop damage, creating a lights-out manufacturing environment that runs continuously through night shifts.
How to Select the Best Glass Engraver for Your Facility
Run through this operational audit before approving equipment specifications:
Assess Wall Thickness: Thin glass (under 1.5 mm) requires UV cold processing. Thick plate glass (above 6 mm) handles industrial CO2 systems if deep frosting is the target.
Quantify Line Takt Time: Calculate how many seconds your workflow permits per piece. High throughput demands galvo heads rather than mechanical gantry heads.
Map Software Interoperability: Confirm the machine controller speaks your factory language, whether that means OPC-UA protocols, standard industrial Ethernet, or automated ERP/MES order imports.
Inspect Structural Rigidity: Glass is heavy. Processing flat panels requires rigid machine frames and vibration-damped toolbeds to prevent optical distortion.
Investing in reliable machinery safeguards your client contracts and shields your brand from line-stoppage penalties. Equipment from established manufacturers like BAINENG CNC provides the mechanical stiffness, optical alignment, and software interfaces needed for consistent, high-yield manufacturing runs.
Frequently Asked Questions
Q1: Why is a UV laser often considered the best glass engraver over a
fiber laser?
A1: Standard fiber lasers operate at an infrared
wavelength of 1064 nm, which passes straight through clear glass without
sufficient energy absorption. Trying to mark glass with a standard fiber source
causes uncontrolled cracking or no visible mark at all. UV lasers (355 nm) are
strongly absorbed by glass, allowing cold, non-thermal processing with zero
thermal fractures.
Q2: Can industrial laser engravers handle curved, conical, or
irregular glass vessels?
A2: Yes. High-performance industrial
systems utilize motorized rotary fixtures synchronized with dynamic 3D galvo
focusing heads. Combined with optical distance sensors or machine vision, the
machine shifts its focal point dynamically over the curved surface, preventing
line stretching or blur.
Q3: How much downtime should a factory expect for routine
maintenance?
A3: Sealed RF-excited CO2 and solid-state diode-pumped
UV laser sources require very little day-to-day maintenance compared to
sandblasting. Standard maintenance involves inspecting chiller water levels,
cleaning external debris-extraction filters, and wiping protective optical
windows. Expect less than two hours of scheduled maintenance per month.
Q4: Can laser engraving weaken tempered glass panels?
A4:
Yes, if executed with the wrong parameters. Tempered glass contains high surface
compression stress. High-heat CO2 systems can penetrate this surface layer,
releasing internal tension and shattering the entire lite. UV laser engraving
removes only microscopic depths (measured in microns) through cold photochemical
ablation, making it safe for tempered glass when calibrated correctly.
Q5: What dust and fume extraction is needed for continuous glass
production?
A5: Laser etching on glass creates sub-micron silicate
dust particles that damage optical mirrors and present a respiratory hazard.
Industrial workcells require dedicated, multi-stage HEPA filtration units with
brushless turbines, integrated directly into the machine controller to run only
during laser firing cycles.
Upgrade Your Glass Processing Facility
Operating legacy machines with high scrap rates compromises your delivery schedules and erodes your operating margins. Upgrading to high-yield commercial laser workstations transforms glass processing into a consistent, automated profit driver.
BAINENG CNC engineers high-precision, automated glass production systems built to withstand the realities of 24/7 factory environments. Contact our applications team today to schedule an engineering review, run test cuts on your proprietary glass materials, or request a complete technical specification packet.