
 FAQs
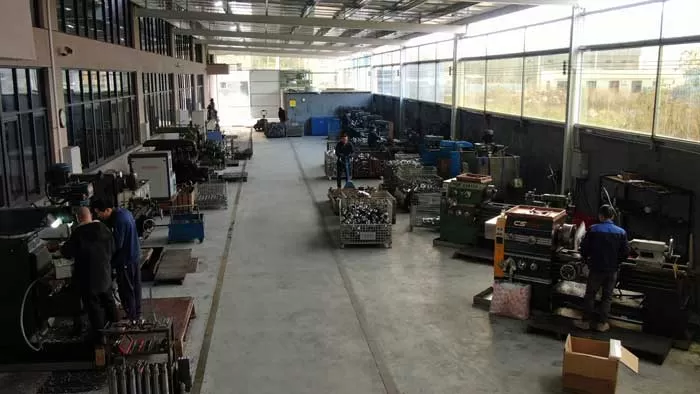
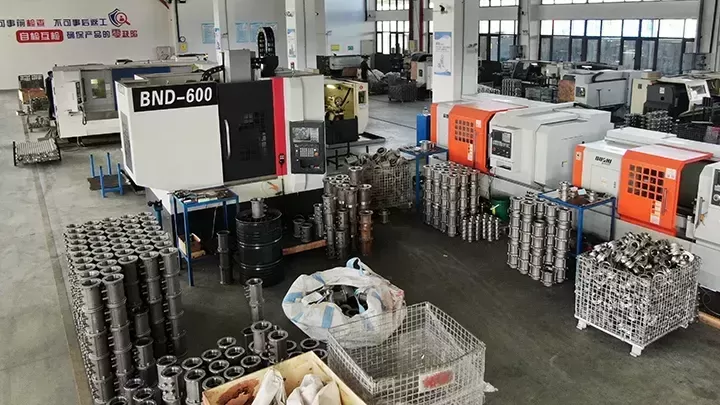
 Factory Tour


The glass fabrication industry has transitioned from manual cutting and etching to fully digitized, computer-controlled production ecosystems. Modern glass manufacturing equipment encompasses a wide array of machinery—from float lines and automatic cutting tables to edging, drilling, washing, tempering, and laminating systems. Within this spectrum, CNC glass engraving and carving equipment represents a pinnacle of precision engineering, enabling high-resolution surface texturing, deep 3D sculpting, and complex edge profiling. This guide provides an authoritative examination of core glass processing machinery, with a technical deep dive into industrial CNC engraving solutions, addressing real-world manufacturing challenges and process optimization strategies.
The Evolution of Glass Manufacturing Technologies
Traditional glass processing relied heavily on manual score-and-snap methods, pantograph engravers, and sandblasting masks—each presenting limitations in repeatability, geometric complexity, and production throughput. The introduction of CNC (Computer Numerical Control) technology in the 1990s revolutionized the industry. Today, integrated glass manufacturing lines combine automated loading, laser measurement, waterjet cutting, and high-speed milling centers. The shift toward Industry 4.0 has further enabled real‑time toolpath optimization, remote diagnostics, and adaptive feedrate control, significantly reducing breakage rates and improving surface finish quality.
First-generation equipment: Manual cutting wheels, straight-line edgers, single-spindle drill presses.
Second-generation (semi-automated): Programmable waterjet cutters, 2.5D engraving routers, PLC‑controlled grinding lines.
Third-generation (fully digital): 5‑axis CNC machining centers, laser‑assisted engraving, AI‑based defect detection, cloud‑connected production cells.
This evolution has made it possible to process float glass, low‑iron glass, laminated glass, and even thin‑film coated panels with micron‑level accuracy. For B2B buyers, understanding the capabilities of each equipment category is critical when designing a production workflow.
Classification of Core Glass Processing Equipment
An efficient glass fabrication plant integrates several machine types. Below is a technical breakdown of key equipment groups:
Primary Cutting & Shape Formation
CNC Cutting Tables: Optimized nesting software, diamond wheel scoring, and pneumatic breaking bars. Typical tolerance ±0.2 mm.
Waterjet Cutting Systems: Abrasive‑assisted cutting for thick glass (up to 50mm), no heat‑affected zone, ideal for intricate shapes.
Laser Cutting (specialized): Used for thin soda‑lime glass and display panels; requires precise thermal management.
Edge Processing & Surface Preparation
Straight‑line edgers: Rough and fine grinding wheels, polishing pads for arrised or flat edges.
Double‑edger machines: Simultaneous processing of two parallel edges, speeds up to 8 m/min.
CNC grinding & polishing centers: 3‑axis or 4‑axis for complex edge profiles (beveled, ogee, pencil).
Drilling & Milling
Vertical drilling machines: Single or multi‑spindle, coolant‑fed diamond drills for holes from 4mm to 50mm.
CNC machining centers (glass routers): Combined drilling, milling, engraving, and countersinking in one setup.
Thermal & Laminating Equipment
Horizontal tempering furnaces (convection or radiation heating).
Autoclaves and vacuum laminators for safety glass (PVB, SGP interlayers).
Heat‑soak testing ovens for nickel sulfide inclusion detection.
Among these categories, CNC glass engraving machines require the highest mechanical stiffness and advanced motion control, as they perform micro‑chipping processes on brittle materials. Equipment from specialized manufacturers like BAINENG CNC integrates high‑torque spindles with active vibration damping to achieve consistent engraving depths.
CNC Glass Engraving: Precision at the Core of Modern Manufacturing
Industrial glass engraving has moved far beyond simple surface etching. Contemporary CNC engravers execute intricate 3D reliefs, micro‑textured patterns, and functional features (e.g., light‑diffusing structures for architectural glass). The process uses diamond‑coated or polycrystalline (PCD) tools rotating at 15,000–30,000 RPM, with a controlled depth of cut typically between 0.05 mm and 2 mm per pass.
Technical Architecture of Professional Glass Engravers
Granite or heavy ribbed cast‑iron base: Provides thermal stability and absorbs high‑frequency vibrations.
Linear guides and precision ball screws: Ensure positioning accuracy of ±0.02 mm across the entire work envelope.
Water‑cooled high‑frequency spindle: 3.5 kW to 7.5 kW, ISO20/HSK‑63 tool interface, runout < 0.005 mm.
Closed‑loop servo drives: Enable real‑time position feedback and jerk‑limited acceleration profiles.
Integrated mist/coolant system: Reduces tool‑glass interface temperature and flushes away fine glass dust.
Automatic tool changer (ATC): With 8–12 tool positions for swapping between roughing, finishing, and chamfering tools.
Typical working sizes range from 600x600 mm (for optical components) up to 2500x4000 mm (for architectural panels). Four‑axis and five‑axis variants allow undercut engraving and oblique edge carving, which are essential for mold manufacturing or decorative curved glass elements.
Application Domains Demanding High‑Precision Engraving
Architectural decorative glass: Floral, geometric, or logo patterns on lobby partitions, balustrades, and elevator doors.
Automotive glass personalization: Anti‑glare micro‑grooves, defroster grid channels, and bespoke sunroof engravings.
Household appliance panels: Oven doors, refrigerator shelves, and washing machine portholes with brand icons or functional markers.
Furniture and interior design: Glass tabletops, cabinet inserts, mirrors with beveled engraved edges.
Scientific and optical glass: Precision alignment marks, fluidic channels for micro‑reactors, and diffractive optical elements.
Technical Parameters and Operational Considerations for Industrial Glass Engraving
Selecting the correct engraving machine for a specific production volume and glass type requires analyzing several key specifications. Below is a professional checklist based on field experience.
Critical Machine Parameters
Spindle power & torque curve: For glass harder than 6 on Mohs scale, low‑end torque at 8,000–12,000 RPM is more important than maximum RPM.
Maximum tool diameter: Typically 8–20 mm for roughing; 1–6 mm for fine engraving (micro‑tools require collet concentricity < 3 μm).
Vacuum worktable design: Segmented vacuum zones allow secure clamping of irregularly shaped glass sheets without mechanical clamping that might cause edge cracks.
Dust extraction capacity: Minimum 3,000 m³/h with HEPA filtration (fine glass particles are hazardous to operators and linear guides).
Coolant management: Closed‑loop filtration with pH‑neutral corrosion inhibitors prevents white stain marks on the engraved surface.
Control software compatibility: Native support for G‑code, HPGL, DXF, and STEP files; post‑processors for popular CAM systems like AlphaCAM, EnRoute, or ArtCAM.
Operators must also consider the glass composition: soda‑lime glass machines differently than borosilicate or aluminosilicate glass. Engraving speeds for 3 mm float glass typically range from 2,000 mm/min to 6,000 mm/min, while 10 mm thick glass requires slower speeds (600–1,500 mm/min) and multiple finishing passes to prevent edge chipping.
Addressing Industry Pain Points with Advanced CNC Solutions
Despite the maturity of glass processing technologies, fabricators consistently face technical hurdles that undermine profitability. Below we analyze common pain points and present engineering solutions implemented in modern CNC engraving platforms, including those developed by BAINENG CNC.
Pain Point 1: Edge Chipping and Surface Micro‑Cracks
Cause: High tool runout, excessive feedrate, lack of
coolant, or inappropriate diamond grit size.
Solution: Use
of precision‑balanced holders, adaptive toolpath strategies (trochoidal
milling), and pulsed coolant application. BAINENG CNC’s engraving series
incorporates real‑time vibration monitoring that automatically reduces feedrate
upon detection of chatter harmonics, consistently reducing chipping rates by
over 40% in field tests.
Pain Point 2: Long Setup Times for Complex Patterns
Cause: Manual tool changes, offline programming
inefficiencies, and non‑integrated workholding.
Solution: Machines with automatic tool changers, quick‑change vacuum pods, and embedded
CAM simulation reduce setup from hours to minutes. An integrated tool library
with preset tool lengths eliminates repetitive measurements.
Pain Point 3: Inconsistent Depth Across Large Panels
Cause: Glass thickness variation (typical ±0.5 mm) and
workpiece warpage.
Solution: Implementation of laser
distance sensors that map the glass topography before engraving; the CNC
controller then dynamically compensates Z‑axis height in real time. This active
mapping ensures uniform engraving depth even on bowed glass.
Pain Point 4: High Tooling Costs and Short Tool Life
Cause: Inadequate feed/speed parameters, improper coolant
concentration, or low‑quality diamond burs.
Solution: Using
tool wear monitoring systems that log spindle load and engraving quality. When
tool wear reaches a threshold, the machine pauses and signals operator
replacement. Combined with optimized chip thinning strategies, tool life can be
extended by 30–50%.
Industrial feedback consistently highlights that vertical integration of control hardware and software—such as that found in BAINENG CNC glass routers—delivers superior process stability compared to generic CNC retrofits. This holistic approach addresses mechanical, electrical, and software interdependencies inherent in glass engraving.
Optimizing Production Workflow: Integrating Engraving with Cutting, Edging, and Drilling
To maximize return on investment, a CNC glass engraver should not operate as an isolated island. A well‑designed production cell sequences operations to minimize handling and re‑positioning errors. A recommended workstream:
Automated loading from storage rack using suction lifters → conveyor to CNC cutting table.
Cutting to net shape with break‑out table → edge inspection.
Edge grinding and polishing (if required) before engraving – prevents embedding of abrasive particles from grinding wheels into engraved channels.
CNC engraving/milling on a dedicated machining center equipped with vacuum table and dust shroud.
Washing and drying inline (deionized water rinse removes glass slurry, avoids water spots).
Tempering or laminating – engraving must be performed before heat treatment (engraving after tempering risks crack propagation).
Data integration through MES (Manufacturing Execution System) enables job tracking, tool life management, and statistical process control. For high‑mix, low‑volume production, quick‑change fixtures and offline programming can reduce changeover times to under 15 minutes.
Future Trends in Glass Manufacturing Automation
Three technological trajectories are set to redefine glass engraving and overall equipment efficiency over the next five years:
AI‑driven adaptive toolpath generation: Machine learning models trained on past engraving results can automatically adjust stepover distances and feedrates to minimize sub‑surface damage, particularly for brittle glasses.
Digital twins for predictive maintenance: Virtual replicas of engraving spindles and drive systems simulate wear patterns. Real sensor data triggers maintenance alerts before catastrophic failures occur.
Collaborative robotics for part handling: Lightweight cobots that assist with flipping large glass panels for double‑sided engraving, reducing manual injury risks and improving cycle times.
Eco‑friendly dry engraving technologies: Cryogenic cooling (liquid nitrogen mist) eliminates wastewater treatment costs while maintaining low temperatures to prevent thermal shock.
Forward‑thinking equipment buyers should prioritize open‑architecture controllers that allow retrofitting of future AI modules and IIoT connectivity. Systems that currently support OPC UA and MQTT protocols will have a longer service life and better interoperability.
Frequently Asked Questions (FAQ)
Q1: What thickness range of glass can a professional CNC engraving machine process?
A1: Industrial CNC glass engravers typically handle thickness from 2 mm up to 25 mm. For very thin glass (<2 mm="">25 mm), multi‑pass engraving with progressive depth increments is recommended. Always verify the machine’s Z‑axis clearance and spindle power for deep carving.
Q2: Can I engrave on already tempered glass?
A2: Engraving on fully tempered glass is strongly discouraged. The surface compressive stress layer (about 2–3% of thickness) will be disrupted, often leading to spontaneous shattering hours or days after engraving. Always perform CNC engraving on annealed or heat‑strengthened glass before the tempering process.
Q3: What is the typical lifetime of a diamond‑coated engraving tool on soda‑lime glass?
A3: Under optimal parameters (feed 3,000 mm/min, depth 0.2 mm, adequate coolant), a quality diamond burr (grit #150–#300) can engrave 1,500–3,000 linear meters before requiring replacement. Factors such as glass composition, coolant contamination, and spindle runout dramatically affect tool life. Implementing tool wear monitoring extends predictable usage.
Q4: Which software file formats are compatible with industrial glass engraving machines?
A4: Most professional controllers accept standard G‑code (ISO 6983), HPGL for 2D vector engraving, DXF for 2.5D pocketing, and STEP/IGES for 3D surface machining. Some proprietary CAM systems output native formats that are later converted. Ensure your machine control supports a post‑processor compatible with your CAD/CAM software (e.g., SolidWorks, RhinoCAM, or ArtCAM).
Q5: How do I prevent white residue or “burn marks” on the engraved glass surface?
A5: White residue is typically caused by inadequate coolant flow or incorrect pH level of the coolant mix. Use a dedicated glass machining fluid (pH 7–9) with a concentration of 6–10%. Mist application should provide full coverage on the tool entry point. For dry engraving, a pulsed air blast with fine water spray significantly reduces thermal buildup. Post‑engraving ultrasonic cleaning removes any remaining debris.
Q6: What maintenance schedule is recommended for a CNC glass router used daily?
A6: Daily: Clean glass dust from linear guides and ball screws, check coolant level and filter condition. Weekly: Lubricate guide rails, inspect spindle collet for wear, verify vacuum table seal integrity. Monthly: Calibrate tool length sensor, measure spindle runout (acceptable<0.008 mm="">
Ready to upgrade your glass processing line with a reliable, high‑precision CNC engraving solution? Whether you need a compact 3‑axis machine for small decorative parts or a large‑format 5‑axis system for architectural glass panels, our engineering team provides tailored recommendations based on your material portfolio, production volume, and budget constraints. Contact BAINENG CNC’s technical sales department for a detailed equipment specification sheet, sample engraving test reports, and a personalized ROI simulation. Submit your project requirements via the online form or email, and expect a response within 24 hours.
Email:kobexu@bai-neng.com | Phone: +86-17185883788 (International hotline) | Request a virtual demo or on‑site trial today.